
What is a Central Control Room ?
A central control room is the main operating point of a waste recycling plant. It integrates key equipment such as sorting lines, conveyors, shredders, and balers into a single control system, usually based on PLC technology. Operators can view the entire process in one place and manage production in a more structured and efficient way.
It is mainly used to monitor running status, manage alarms, and adjust equipment operation when necessary. By reducing on-site manual intervention and providing clearer system feedback, it helps the plant run more stably and reduces downtime caused by missed signals or delayed responses.
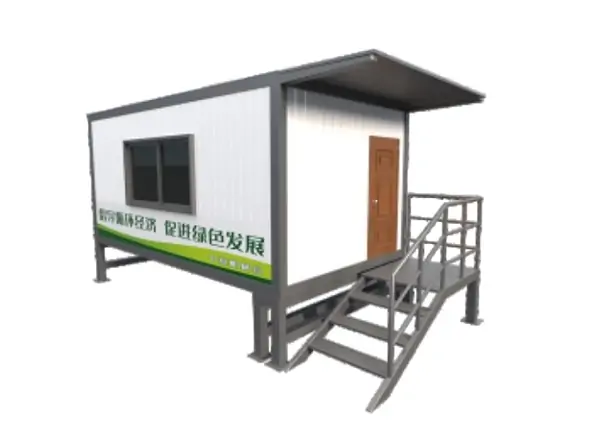
Working principle
A smart control room serves as the central control hub of a recycling plant. It collects real-time data from connected equipment, processes information through the PLC system, and sends control commands to coordinate plant operations, ensuring stable production, efficient material flow, and rapid response to system abnormalities.
Data Collection : Sensors, motors, conveyors, and sorting equipment continuously send operating data to the control room, providing real-time visibility of plant conditions.
Control Logic Processing : The PLC analyzes incoming data based on predefined operating parameters and process requirements, then determines the appropriate control actions.
Equipment Command Execution : Control signals are transmitted to conveyors, shredders, balers, fans, and other equipment, ensuring coordinated operation throughout the recycling process.
Continuous System Optimization : The monitoring and control cycle runs continuously, helping operators improve efficiency, reduce downtime, and maintain stable plant performance.
Features
A central control room helps operators monitor equipment, manage production, and maintain stable plant operation from a single location.A central control room helps operators monitor equipment, manage production, and maintain stable plant operation from a single location. Xinzhongyi ECO combines control system engineering, equipment integration, PLC programming, and plant automation expertise to deliver complete recycling plant solutions from design through commissioning.
Equipment Monitoring
Monitor conveyors, sorting equipment, shredders, baler machines, and other key machines in real time. Operators can quickly check equipment status and production conditions across the entire plant.
Plant Operation Control
Control and coordinate equipment throughout the recycling process from one system. This helps maintain smooth material flow and stable plant performance.
Alarm & Fault Management
Automatically detect equipment faults, overloads, blockages, and emergency stops. Early warnings allow operators to respond quickly and reduce downtime.
Production Data Recording
Record processing capacity, equipment runtime, production output, and downtime data. These records help support performance evaluation and maintenance planning.
Parts of Smart Control Room
A smart control room combines industrial automation hardware and monitoring software to manage equipment, production data, and plant operations from a centralized location.
PLC Control System: The core controller of the recycling plant. It receives signals from sensors and equipment, then automatically controls conveyors, sorting systems, shredders, balers, and other machinery according to the programmed operating logic.
SCADA Monitoring System: Provides a real-time overview of plant operation through graphical dashboards. Operators can monitor equipment status, production flow, alarms, and key performance data from a single interface.
Human-Machine Interface (HMI): Touchscreen panels allow operators to start or stop equipment, adjust operating parameters, view alarms, and access production information quickly and easily.
Variable Frequency Drives (VFDs): Control the speed of motors used in conveyors, fans, pumps, and other equipment. VFDs help optimize energy consumption, reduce mechanical wear, and improve process stability.
Sensors and Field Instruments: Collect real-time data such as motor load, conveyor speed, material level, temperature, and equipment status, providing accurate information for automated control and monitoring.
Alarm and Safety Protection Devices: Include circuit breakers, overload protection, emergency stop systems, and fault alarms. These components help protect equipment, improve plant safety, and reduce unexpected downtime.
Specifications
The technical configuration of a smart control room varies according to plant capacity, equipment quantity, and automation requirements. Factors such as cabinet construction, protection level, electrical load, control voltage, and communication architecture are selected based on the operating environment and process demands of each recycling facility. The following specifications represent typical configurations used in municipal solid waste, RDF, SRF, and resource recovery plants.
| Parameter | Typical Specification |
| Protection Rating | IP32–IP65 |
| Rated Voltage | AC 380V / 400V / 415V |
| Rated Current | Up to 1000A |
| PLC System | Siemens, Schneider, ABB or Equivalent |
| Communication Protocol | Modbus, Profinet, Ethernet/IP, OPC UA |
| Remote Monitoring | Available |
Advantages
Applications
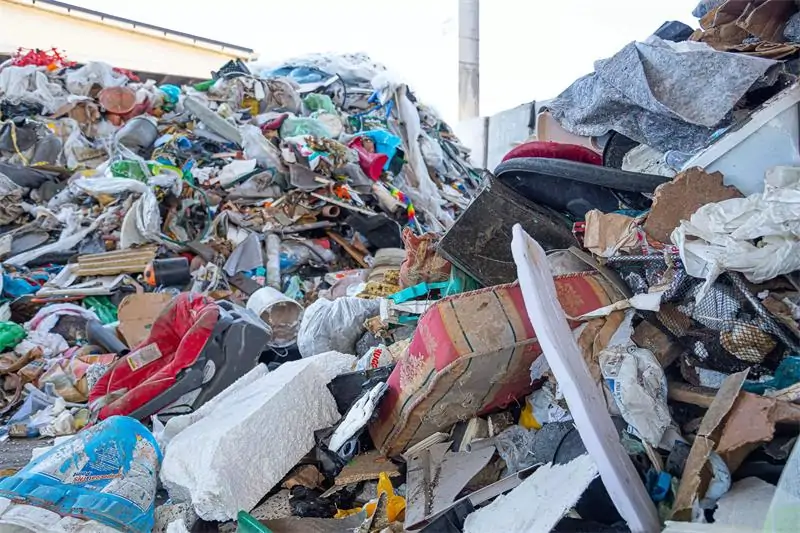
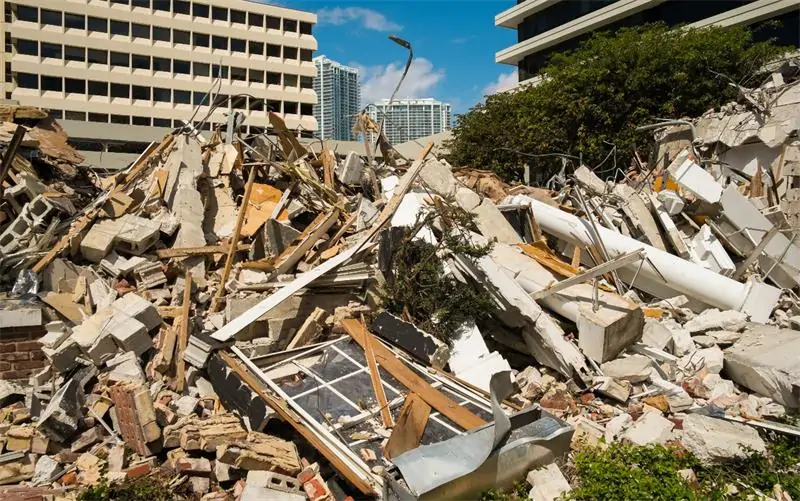
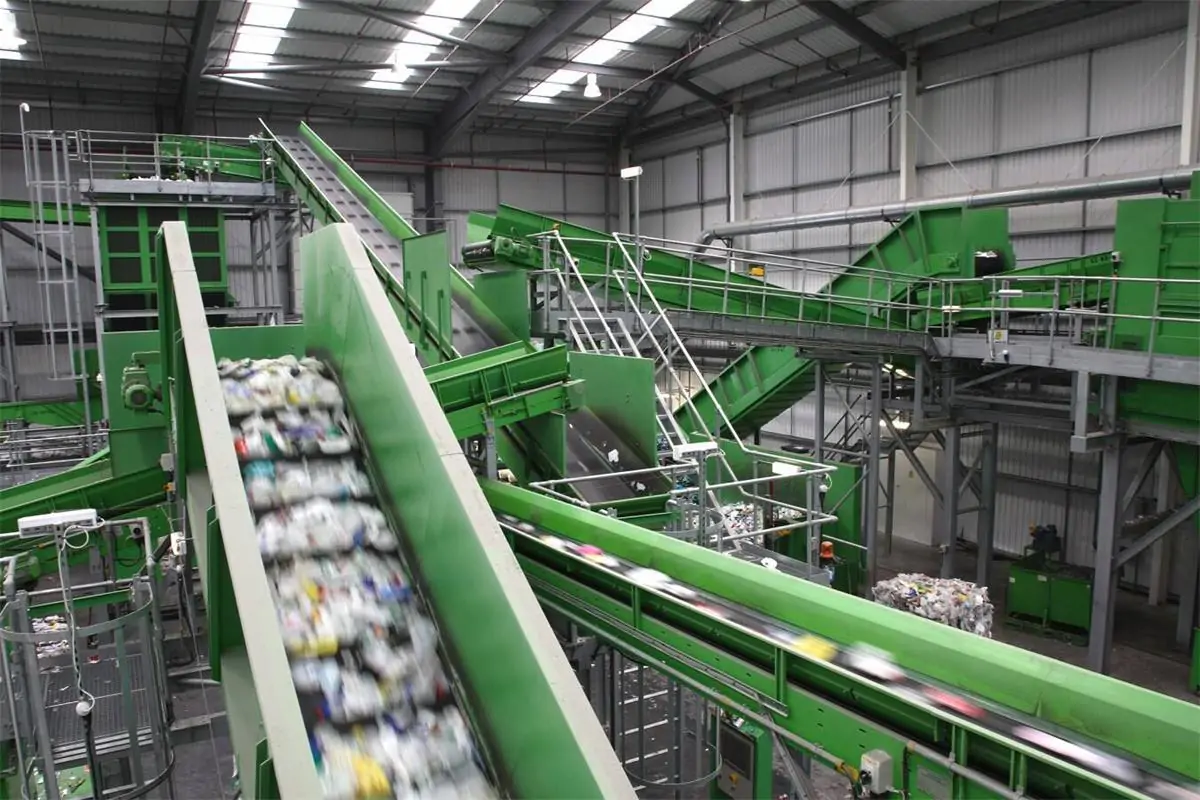
Smart control rooms are widely used in recycling facilities that require centralized equipment management, real-time monitoring, and automated process control. They support various waste treatment and resource recovery applications, helping improve operational efficiency and plant reliability.
Custom Engineering Solutions
Xinzhongyi ECO designs central control cabinet systems for waste recycling plants based on actual site requirements, including MSW, C&D waste, RDF, SRF, and plastic recycling projects. Each control system is configured according to equipment layout, number of control points, and plant capacity to ensure stable operation of the whole recycling line.
The control cabinet integrates PLC-based control of conveyors, sorting equipment, shredders, balers, and auxiliary machines. It ensures reliable signal exchange and coordinated operation between all connected equipment, keeping the production line running in a stable and continuous manner.
Central Control Room System Manufacturer & Supplier
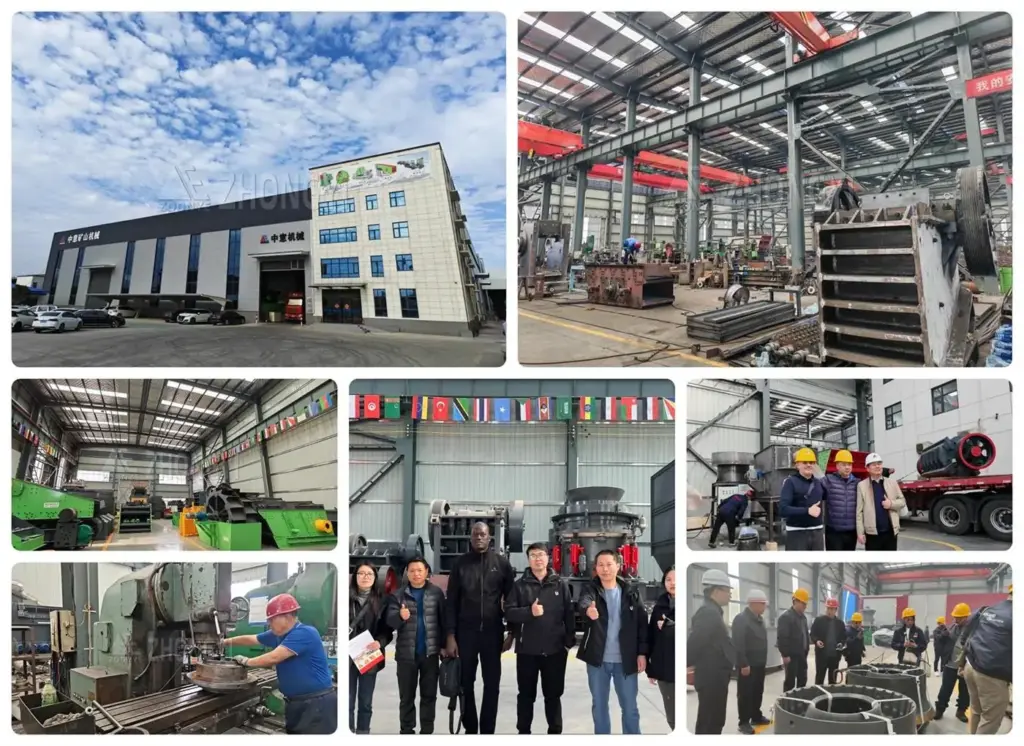
With 16 years of experience in recycling plant automation, Xinzhongyi ECO is a direct manufacturer and system supplier, not a trading company. We design and deliver complete plant automation and control systems, covering engineering design, manufacturing, integration, installation, and commissioning.
Xinzhongyi ECO focuses on practical, project-driven solutions that ensure stable operation, easy system management, and scalable expansion. Our one-stop production line solutions are built to meet real on-site requirements, helping customers improve efficiency, reduce operational risk, and support long-term plant development.
FAQ
A central control cabinet integrates PLC, relays, and protection systems to manage and coordinate all equipment in a recycling line, ensuring stable and automated operation.
It enables real-time control and synchronization of conveyors, shredders, and sorting systems, reducing downtime and improving overall production efficiency.
Yes, it is fully customizable based on plant layout, capacity, material type (MSW, C&D, RDF), and automation level requirements.
It includes overload protection, emergency stop systems, fault alarms, and interlock logic to prevent equipment damage and operator risk.
Yes, modern central control cabinets can support SCADA systems or IoT-based remote monitoring for real-time data tracking and diagnostics.
Regular inspection of wiring, cooling system, PLC status, and dust protection is required to ensure long-term stable operation.