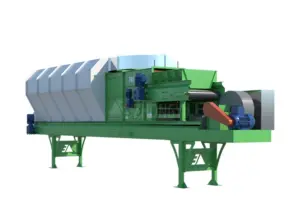



What is an Enclosed Belt Conveyor?
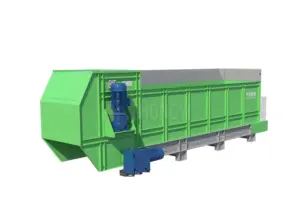
An Enclosed Belt Conveyor is designed for the transportation of sludge, municipal solid waste, RDF/SRF, biomass, and other difficult materials in environmental processing plants. Its fully enclosed structure helps contain dust, odors, and material leakage, reducing secondary pollution and supporting compliance with strict environmental standards.
Built for harsh operating conditions, this Waste Recycling Conveyor can be equipped with corrosion-resistant materials, anti-clogging devices, and automated control systems. It is widely used in waste treatment plants, sewage facilities, recycling centers, and industrial waste processing lines where clean, reliable, and continuous conveying is required.


หลักการทำงาน
An Enclosed Belt Conveyor transports materials through a continuously moving belt inside a sealed conveying chamber. Designed for waste recycling, sludge handling, RDF/SRF production, and other environmental applications, it combines enclosed conveying, dust control, and intelligent monitoring to achieve clean, stable, and efficient material transfer throughout the production process.
Material Feeding: Waste materials are discharged into the conveyor through hoppers, chutes, or feeding equipment, ensuring a controlled and continuous material flow.
Belt Conveying: A motor-driven pulley rotates the conveyor belt, carrying materials along the enclosed conveyor route from the loading point to the designated discharge area.
Dust & Leakage Control: The fully enclosed housing, combined with optional negative-pressure dust extraction systems, prevents dust escape, odor diffusion, and material spillage during transportation.
Intelligent Monitoring: Sensors continuously track belt alignment, tension, bearing condition, and motor temperature, providing early warnings and helping maintain stable operation with reduced downtime.
Parts of Enclosed Belt Conveyor Machine
High-end Enclosed Belt Conveyors used in environmental and recycling industries are designed for dust control, corrosion resistance, and reliable continuous operation. Each component is selected according to material characteristics, operating conditions, and environmental requirements to ensure stable conveying performance and long service life.
Conveyor Belt: Carries materials safely, resisting corrosion, heat, and sticking for reliable transport.
Idlers & Rollers: Support the belt, absorb impact, and maintain smooth movement under harsh conditions.
Drive & Return Rollers: Transfer power and guide the belt while preventing slippage and wear.
Enclosed Cover & Dust Control System: Contains dust, odors, and prevents material leakage during conveying.
PLC Control System: Monitors operation and adjusts parameters for safe, continuous, and efficient running.
Tensioning Device: Keeps the belt properly tensioned to ensure stable long-distance operation.
Belt Cleaner: Removes residual material to reduce buildup, maintenance, and cleaning frequency.

Benefits of Enclosed Belt Conveyor
High-end Enclosed Belt Conveyors deliver stable, dust-free, and corrosion-resistant material handling for environmental and recycling facilities, combining sealed design, durable materials, and intelligent monitoring for efficient, compliant operation.
วัสดุที่ใช้งานได้
High-end Enclosed Belt Conveyors handle diverse materials, including sludge, municipal waste, RDF/SRF, tailings, biomass, and chemical residues, with properties like high moisture, stickiness, abrasiveness, and corrosiveness.
Video Show
Specifications
The following specifications are for reference. Conveyor length, belt width, capacity, enclosure structure, and drive configuration can be customized to suit your material characteristics and site requirements.
| Item | Specification |
|---|---|
| Conveyor Type | Enclosed Belt Conveyor |
| Belt Width | 500-2000 mm |
| Conveyor Length | 5-100 m (Customizable) |
| Capacity | 50-3000 TPH |
| Belt Speed | 0.8-3.15 m/s |
| Inclination Angle | 0-18° |
| Material Size | ≤300 mm |
| Drive Power | 2.2-250 kW |
| Cover Type | Fully Enclosed Steel Cover |
| Belt Material | Rubber Belt / Heat-Resistant Belt / Oil-Resistant Belt |
| Frame Material | Carbon Steel / Stainless Steel |
| Operating Temperature | -20°C to +80°C |
| Dust Control Efficiency | Up to 95% Dust Containment |
| Installation Type | Fixed / Modular Design |
| การใช้งาน | Mining, Aggregate, Cement, Port, Power Plant, Chemical Industry |
Enclosed Belt Conveyor vs Conventional Belt Conveyor
Both enclosed and conventional belt conveyors are widely used for bulk material handling. The main difference lies in environmental protection and material containment. A conventional belt conveyor features an open structure, making it suitable for general conveying applications with easy access for maintenance. An enclosed belt conveyor incorporates a protective cover system that minimizes dust emissions, prevents material spillage, and shields conveyed materials from wind, rain, and external contamination. It is particularly suitable for mining, ports, power plants, cement plants, and environmentally sensitive projects.
| Comparison Item | Enclosed Belt Conveyor | Conventional Belt Conveyor |
|---|---|---|
| Structure | Fully or partially enclosed | Open-frame design |
| Dust Control | Excellent, significantly reduces dust emissions | Limited dust control |
| Material Spillage | Minimal | Higher risk of spillage |
| Weather Protection | Protects materials from rain, wind, and sunlight | Materials exposed to weather conditions |
| Environmental Compliance | Suitable for strict environmental regulations | May require additional dust suppression systems |
| Material Loss | Lower material loss during transport | Greater potential for material loss |
| Maintenance Access | Requires opening cover sections | Direct and convenient access |
| Initial Investment | Higher | Lower |
| Operating Environment | Dust-sensitive, outdoor, and long-distance applications | General industrial conveying applications |
| วัสดุที่เหมาะสม | Coal, ore, cement, fly ash, sand, aggregates, fertilizers | Most bulk and packaged materials |
| Safety Performance | Better personnel and equipment protection | Standard protection level |
| Total Lifecycle Cost | Lower in high-dust applications due to reduced cleanup and material loss | Lower initial cost but higher environmental management costs |
Selection Recommendation
Choose an Enclosed Belt Conveyor when dust control, environmental compliance, material protection, or long-distance outdoor conveying is a priority. For standard conveying applications with less stringent environmental requirements, a Conventional Belt Conveyor remains a cost-effective solution.
How to Choose the Right Enclosed Belt Conveyor?
Selecting an Enclosed Belt Conveyor for environmental projects requires focusing on sealing performance, material adaptability, system stability, and manufacturer capability. Priority should be given to dust control, customization, and long-term operating cost rather than only initial price.
Applications
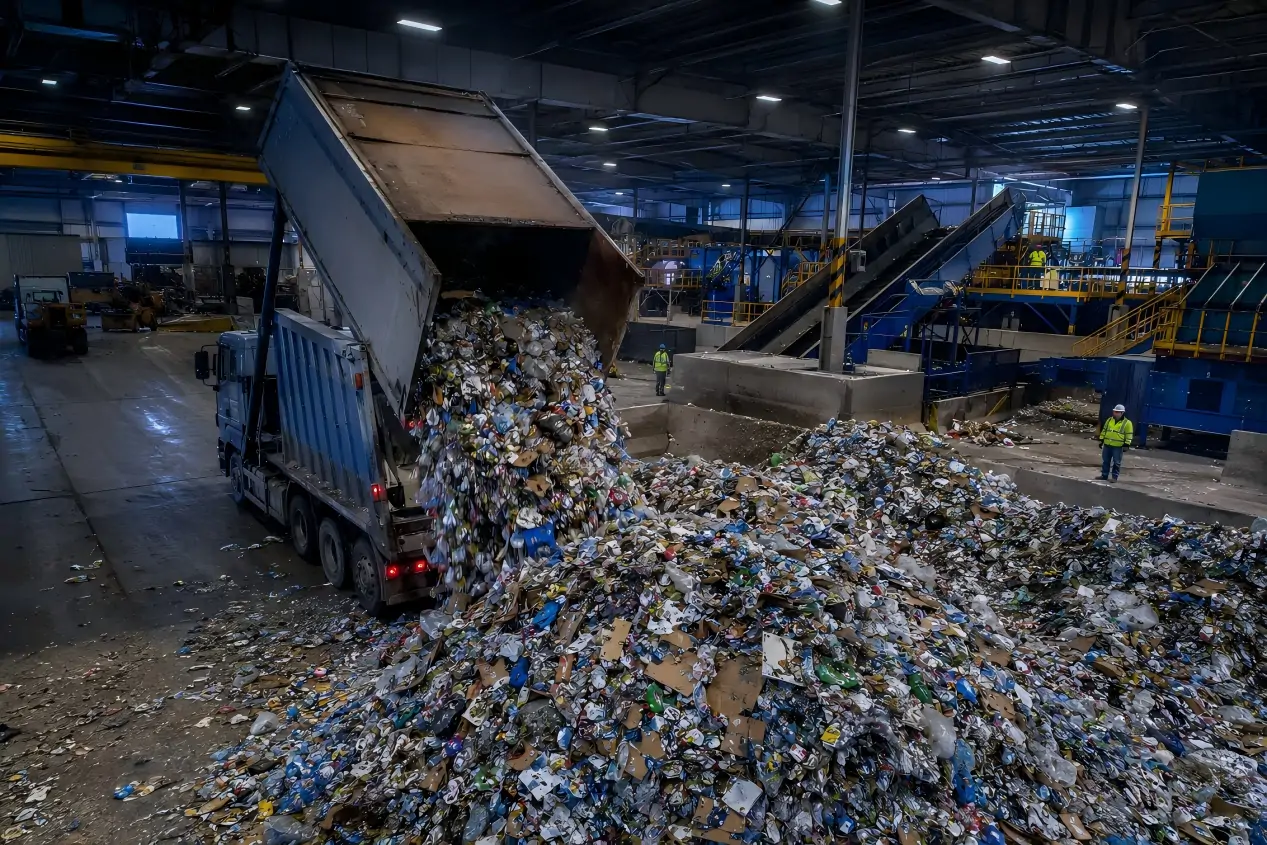
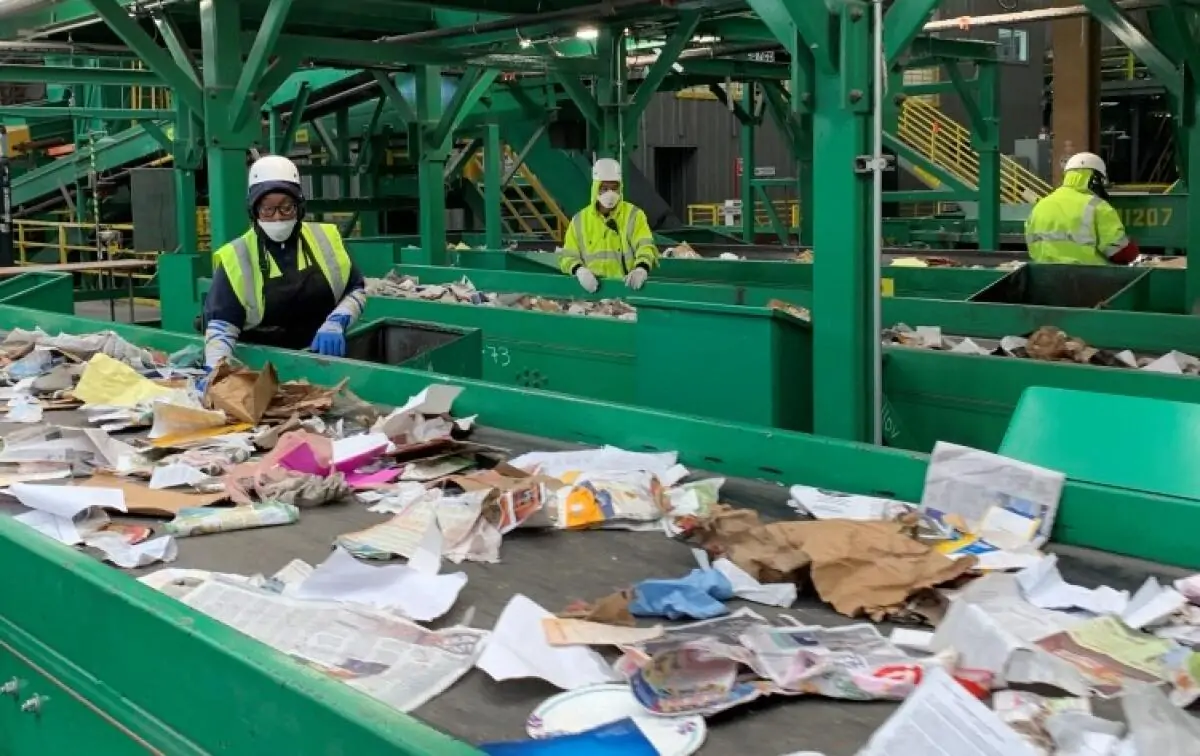
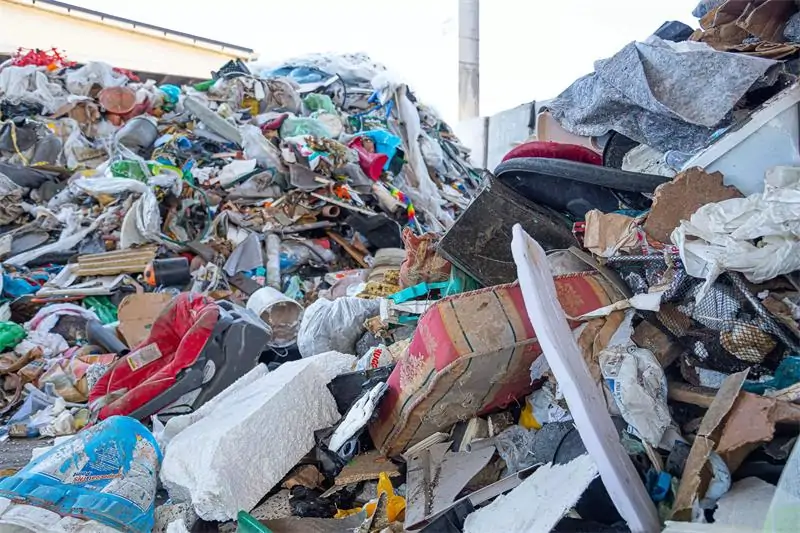
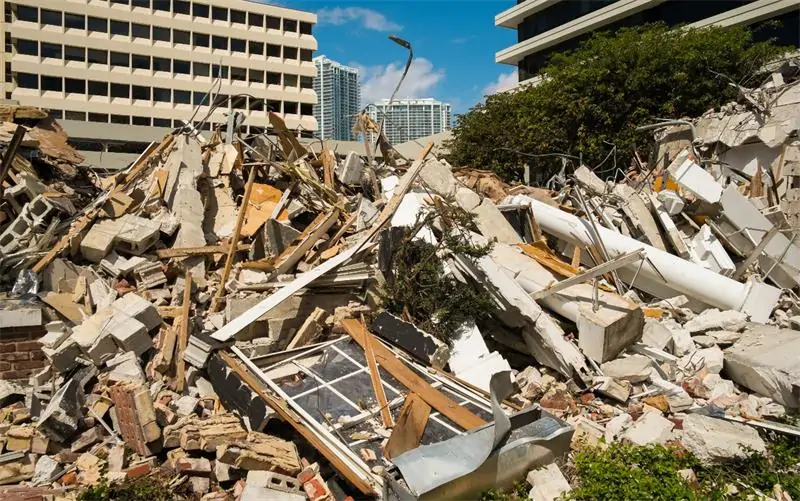
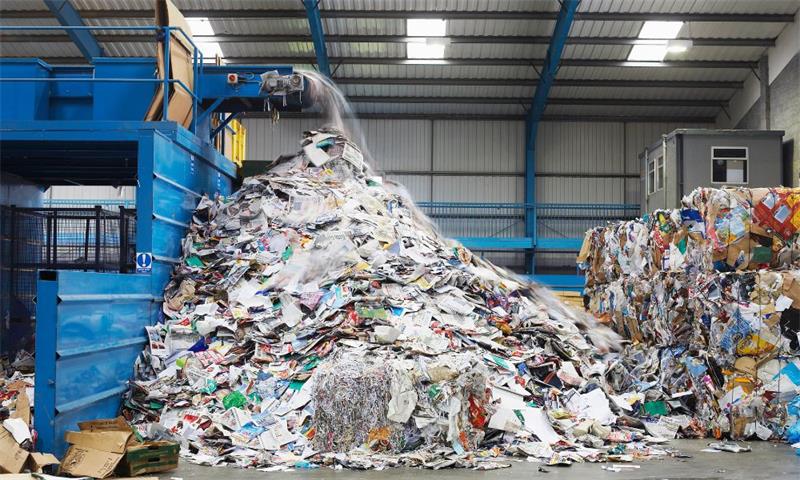
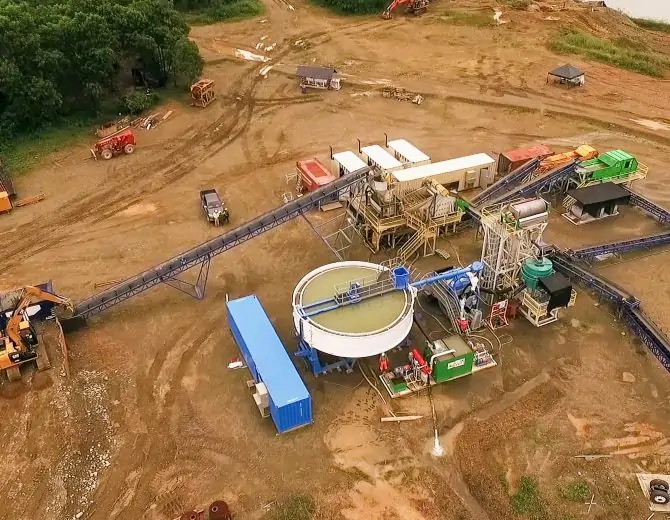
High-end Enclosed Belt Conveyors handle sludge, MSW, RDF/SRF, biomass, tailings, and industrial residues with high moisture, stickiness, corrosion, and dust. They are widely used in waste recycling plants, RDF production lines, biomass processing, waste-to-energy facilities, construction waste recycling, and metal recovery systems for stable and clean conveying.
Custom Enclosed Belt Conveyor Solutions
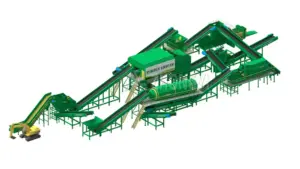
We provide tailored Enclosed Belt Conveyor systems designed to meet the specific characteristics of your materials, processing capacity, and plant layout. Each conveyor is configured according to operational conditions and can function as a standalone unit or be fully integrated into a complete recycling or waste handling line. Contact us with your project details so we can develop a customized solution for your facility.
Custom Options Include:
- กำลังการผลิต: 10–500 tons per day, adjustable to material type and throughput requirements
- Belt and Drive Configuration: Selection of belt type, width, speed, and drive power for optimal material handling
- Incline and Routing: Standard or steep-incline conveyors, with layouts adapted to plant geometry and transfer points
- Sealing and Dust Control: Fully enclosed structures, negative-pressure dust extraction, and odor control systems
- Automation & Monitoring: PLC control, belt tension sensors, run deviation detection, and remote monitoring for predictive maintenance
Enclosed Belt Conveyor Manufacturer & Supplier
Xinzhongyi ECO has 16 years of experience in designing and manufacturing high-end Enclosed Belt Conveyors. As both a manufacturer and supplier, we deliver reliable, durable, and efficient equipment tailored for recycling, waste-to-energy, biomass, and industrial residue handling applications. Our conveyors are engineered to meet strict environmental standards, ensuring dust-free, corrosion-resistant, and stable operation.
We offer complete, one-stop production line solutions, from design and fabrication to installation and commissioning. Xinzhongyi ECO’s professional service team provides on-site support, customized layouts, and intelligent monitoring options, helping clients reduce operational costs, improve safety, and achieve long-term efficiency in material handling.
คำถามที่พบบ่อย
A: เหมาะสำหรับ MSW, RDF/SRF, สลัดจ์, ชีวมวล, หางแร่ และของเสียอุตสาหกรรมที่มีความชื้นสูง ฝุ่น หรือมีคุณสมบัติกัดกร่อน.
A: ใช่ สามารถปรับแต่งได้อย่างเต็มที่ทั้งความยาว ความกว้าง ความจุ มุมเอียง และรูปแบบการติดตั้งตามสภาพหน้างาน.
A: โครงสร้างแบบปิดสนิทผสานกับการซีลและระบบดักฝุ่นแบบแรงดันลบ (ตัวเลือกเสริม) ช่วยป้องกันการรั่วไหลของฝุ่นและการแพร่กระจายของกลิ่น.
A: ใช่ การออกแบบแบบปิดล้อมช่วยปกป้องระบบจากฝน ลม และสภาพแวดล้อมที่รุนแรงเพื่อการทำงานที่มั่นคง.
A: ด้วยชิ้นส่วนที่ทนต่อการสึกหรอและการตรวจสอบอัจฉริยะ ความถี่ในการบำรุงรักษาจึงลดลงอย่างมีนัยสำคัญเมื่อเทียบกับสายพานลำเลียงแบบเปิด.
A: ได้ครับ/ค่ะ มันสามารถเชื่อมต่อกับเครื่องฉีก เครื่องคัดแยก และเครื่องอัดก้อน เพื่อสร้างสายการผลิตการรีไซเคิลขยะที่สมบูรณ์ได้.
A: We are a 16-year manufacturer offering full turnkey solutions, from design and production to installation and after-sales support.